Survey
* Your assessment is very important for improving the work of artificial intelligence, which forms the content of this project
* Your assessment is very important for improving the work of artificial intelligence, which forms the content of this project
The Selection Process
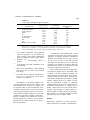
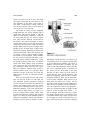
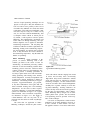
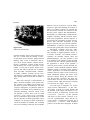
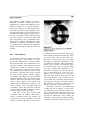
environments and the graphite makes the plastic self-lubricating. Carbon-graphites were not
used because of availability problems. The polyimide molding resin selected cost $9 per pound,
but there are about 400 parts per pound. The material cost per roller is only about 2 cents.
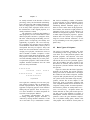
Material: Injection molding polyimide +
20% graphite; shall be ARUN grade 407.
Poly Plastics, Henrietta, NY.
747
lium copper would involve more process steps. It
would have to be heat treated. Wrought spring
materials such as full-hard cold-rolled wrought
steel or copper alloys were considered, but heattreated springs last longer and are more likely to
deliver the desired 107 cycles.
Material: 1080 steel, hardened and tempered
to spring condition (47 HRC). Fabricate
complete and black oxide coat all over.
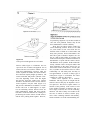
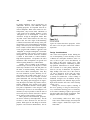
Problem
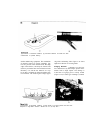
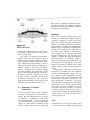
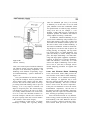
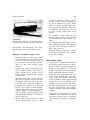
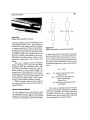
Flat springs are needed to hold plastic film sampIes against a platen in a test rig. The springs are
0.5 mm thick, 10 mm wide, and 50 mm long. A
material is needed for these springs.
Requirements:
l.
Must properties: Black color, will not rust in
50% RH, 70° F room environment.
2. Want properties: Would like 107 flexes at a
stress level of 3000 psi (20.68 MPa).
3. Quantity: Twenty springs.
4. Delivery: Springs must be made within
30 days.
5. SelVice life: The 107 flexes equate to about a
year service life.
6. Cost: Should not cost more than $10 each
after fabrication.
Availability controls this selection to a significant degree. There are not many materials in
warehouses in the form of 0.5-mm-thick sheet
or strip. Two common flat spring materials that
have good availability are 1080 steel and beryllium copper. We opted for 1080 hardened and
tempered spring material. It can be easily blackened with a black oxide treatment. This spring
stock is widely used for flat springs, steel rule
dies, and pallet banding. The springs can be cut
from the hardened strip with a water jet laden
with particles or by EDM machining. The beryl-
Summary
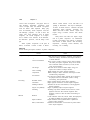
Our discussions of various material systems
should have supplied enough information so that
the designer can quantitatively compare the candid ate materials and know what heat treatments
and processing to use when specifying the material on the drawing. Obviously, it is not possible to compile a list of all the components that
are found on machines. Similarly, the materials listed are not the only ones that will work,
but the examples reflect a wide range of service
experience.
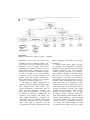
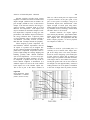
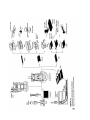
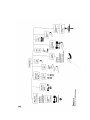
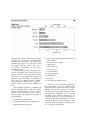
The material selection process should be
started as early as possible in a machine or structure design. The key to proper material selection is to establish a checklist of the properties
required for a serviceable design. Does the part
have to be hard? Does it require corrosion resistance? Are any special physical properties required? Once the required use properties are established and prioritized, designers can draw on
their repertoire of available engineering materials to select one or more candidate materials and
treatments.
Remember to state the function of the
part. What does it do? What are the apparent forces on it? What are the potential unforeseen forces? Calculate stresses based upon
the perceived forces. List potential corrodents;
determine if tribological properties are to be a
consideration. Doing these steps should lead to